- Hydrotesting proves strength, while leak testing proves the completed system is tight in its final configuration.
- A helium tracer in nitrogen lets sniffer detectors locate small leaks at flanges, valves and fittings.
- A flange management system identifies every joint broken after hydrotesting and defines the leak test scope.
- Organising tests by test pack aligns leak testing with the start-up sequence operations need.
A plant that has passed its hydrotests can still leak on start-up. Hydrotesting proves strength, but many systems are then broken open again: spool pieces removed for dewatering, instruments fitted after the test, flanges disturbed for blinds and spades, valves replaced. Each reinstated joint is a potential leak path that has never seen pressure in its final configuration, and hydrocarbon leaks from those joints during start-up are among the most avoidable incidents a project can have.
Service or leak testing with nitrogen, often with a helium tracer, closes that gap. It checks the system as it will run, at a pressure set by the test procedure, before any hydrocarbon arrives.
Why test again after hydrotesting
Hydrotesting and leak testing answer different questions. A hydrotest confirms that pipework and welds can withstand the test pressure defined by the governing code. A leak test confirms that the completed system, including every flange, threaded connection, valve gland and instrument fitting, is tight. Gas finds leak paths that water may not, which is why gas leak testing catches the weeping flanges and fittings a hydrotest can miss, as well as joints that were never part of the hydrotest at all.
Why nitrogen and helium
Nitrogen is inert, dry and readily available, making it a safe medium for pressurising systems that will later carry hydrocarbons. Adding a proportion of helium creates a tracer. Helium is a small molecule that passes readily through leak paths and is present in normal air only at very low levels, so a sensitive detector can pick it out above background. The mix proportion, test pressure and acceptance criteria are set by the leak test procedure and the operator's requirements, reflecting the design and operating conditions of each system.
Every joint you open after the hydrotest is a joint you have not yet tested.
Finding leaks with sniffers
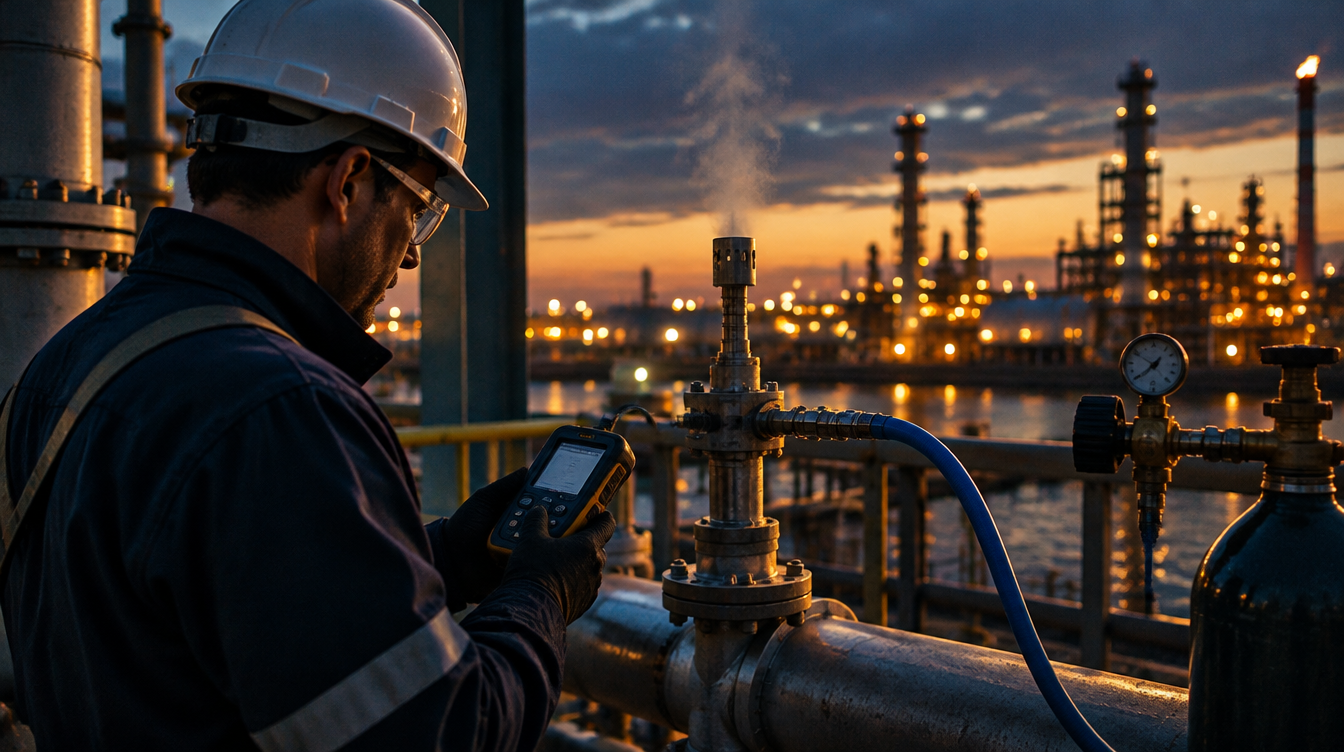
Once a system is pressurised and stable, technicians check each joint with a helium detector, moving a sniffer probe around flanges, valve stems, bonnets, instrument fittings and threaded connections. Flanges are often wrapped with tape around the circumference and a small hole made in it, so that helium escaping from the gasket accumulates and can be detected at the hole. Leaks are logged and tagged, then rectified after depressurisation, and the joint is retested. A pressure hold can be used alongside sniffing as an overall indicator of system tightness.
Wind, heat and open plant areas affect detection, so procedures should account for local conditions. In a Gulf summer, the timing of testing and the safety of technicians working in exposed areas need planning as well.
Flange management makes the difference
Most start-up leaks occur at bolted joints, and most of those trace back to how the joint was made. A flange management system tracks every joint through its life:
- Joint register: a unique identifier for each flange, linked to drawings and test packs.
- Correct components: gasket type, bolt material and lubricant verified against the specification before assembly.
- Controlled tightening: torque or tensioning to specified values by competent technicians, with records kept.
- Break and remake tracking: every joint opened after hydrotesting identified and included in the leak test scope.
- Tagging: physical tags on each joint showing its status, from assembled through to leak tested.
With this in place, the leak test becomes confirmation rather than discovery.
Sequencing by test packs
Leak testing is organised by test packs, each covering a defined system with clear boundaries, isolations and joint lists. Sequencing them in line with the start-up plan lets systems be handed over in the order operations need them. A typical flow is:
- Define test pack boundaries and compile the joint list from the flange register.
- Confirm all joints are complete, tagged and tightened, and that isolations are in place.
- Pressurise in stages with the nitrogen-helium mix to the pressure set by the procedure.
- Check every joint with the detector and record any leaks.
- Depressurise, rectify and retest leaking joints, then close out the pack.
Safety controls matter throughout. A pressurised gas system stores far more energy than a liquid-filled one at the same pressure, so exclusion zones, staged pressurisation and controlled venting are essential, together with the same oxygen-deficiency precautions that apply to any nitrogen work.
A practical first step
Check whether your flange register can tell you exactly which joints have been broken since hydrotesting. If it cannot, start there, because that list defines your leak test scope. KARR's nitrogen services team can help plan test packs or carry out the testing when the time comes.
Leak testing, Helium, Flange management